
Sandblasting (unified texture)
It is used to reduce the graininess of the powder surface and unify the matte texture; it is more suitable for delivering purpose parts and functional parts with a cleaner appearance.
HP MJF Nylon PA12-Dyed Black based on HP MJF process, its advantages lie in "batch consistency" and "dimensional stability."
Quote checklist: Upload your 3D model and, when available, a 2D drawing. Identify the required process, material, quantity, critical dimensions, finish, appearance standard, and target delivery date.
Engineering note: Values below are typical reference ranges. Final manufacturability, tolerances, material condition, surface finish, cost, and lead time depend on the drawing, geometry, quantity, and selected process.
Upload CAD files and mark critical features for an engineering review before production.
| Process | HP MJF 3D printing (nylon powder molding) |
|---|---|
| Color | Black (more resistant to dirt, suitable for on-site use and delivery; sandblasting/painting optional if a uniform texture is required) |
| Dimensional accuracy | ±0.2 mm (common reference; for critical assembly dimensions, it is recommended to mark tolerances in 2D drawings and note "key dimensions first") |
| Minimum wall thickness | 0.8mm (common reference; it is recommended to thicken or reinforce the stress-bearing structure) |
| Service temperature | About 120℃ (common reference; continuous high temperature/long-term thermal load is recommended to explain the working conditions for evaluation) |
| Tensile strength | 45–55 MPa (common range; related to structure orientation/density/finishing) |
| Density | About 1.02 g/cm³ |
| Typical advantages | Stronger batch consistency and better dimensional stability, suitable for delivery of repetitive parts and low- to medium-volume production of functional parts |
| Structure tag | Structural validation/lightweighting |
| Assembly enhancements | support Threaded inserts; Please indicate the thread specification (such as M2/M3/M4), quantity and location; please note if you need to enlarge/ream/tapping |
| Finishing | Sandblasting, threaded inserts, and painting |
| Typical lead time | Related to size, quantity, typesetting and finishing; clear delivery and expedited options will be given after uploading the file |
It is used to reduce the graininess of the powder surface and unify the matte texture; it is more suitable for delivering purpose parts and functional parts with a cleaner appearance.
Used to improve color consistency and surface protection; it is recommended to note the target texture (matte/semi-matte/high-gloss) and reference image.
Used for screw assembly and repeated disassembly; suitable for functional parts such as jigs, brackets, and positioning parts that require higher assembly reliability.
Suitable for parallel production of multiple pieces and delivery of duplicate parts; more friendly to low- to medium-volume production of functional parts, with less rework and fluctuations.
It is more "stable" when used to assemble positioning parts, structural validation parts, and fixtures; it is recommended to mark tolerances on key dimensions and note "key dimensions first".
It is used for equipment peripheral parts, tooling fixtures, and exposed functional parts to be delivered more attractively; if a more uniform appearance is required, sandblasting or painting can be selected.
support Threaded inserts Improves the reliability of screw connections and is suitable for structural parts that need to be fixed/repeatedly disassembled.
| Material | Key Advantages | Mainly applicable | Not suitable |
|---|---|---|---|
| White Nylon (SLS) | The functional type is more stable, does not require support, and is suitable for complex structures and low- to medium-volume typesetting. | Structural validation, assembly parts, wear-resistant moving parts, small batch functional parts | Ultimate mirror appearance, ultra-high precision fit (requires secondary processing/process change) |
| Black Nylon (SLS) | Functional + black stain-resistant; suitable for functional parts with color requirements | Assembly parts, structural parts, wear-resistant parts, batch functional parts | The ultimate mirror appearance and high-precision combination |
| HP Nylon - Gray (MJF) | Better batch consistency and dimensional stability, suitable for repeated delivery | Small and medium batch functional parts, assembly positioning parts, repetitive parts | Ultimate mirror appearance (still needs spray coating/finishing) |
| HP Nylon & Fiberglass - Gray (MJF GF) | Stronger rigidity and dimensional stability, suitable for load-bearing structural parts/positioning parts | Load-bearing structural parts, assembly positioning parts, functional parts with priority on dimensional stability | Fasteners that require a certain degree of elasticity/toughness (needs evaluation) |
| Tough SLA - Yellow-Green (SLA) | A more refined appearance with greater detail; and more impact resistant than standard resins | Appearance + prototype with certain toughness, buckle verification, light load function verification | Complex structure mass layout, wear-resistant for long-term use (better with nylon) |
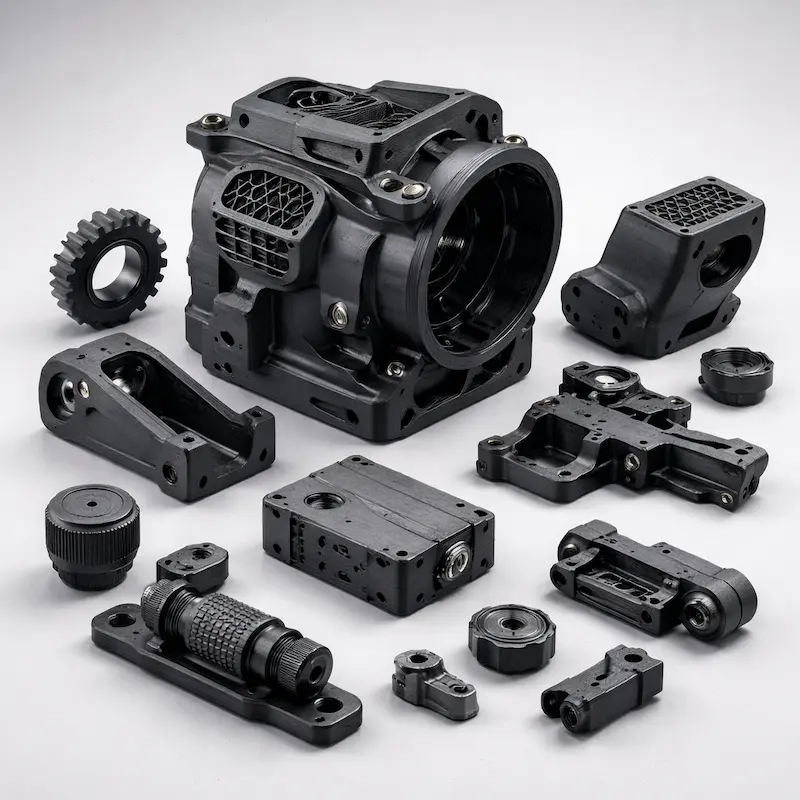
HP Black Nylon (MJF) is more focused on "delivery of functional parts". Typical applications include: assembly parts, positioning parts, jigs and fixtures, and low- to medium-volume repetitive parts.
If you are looking for a “detailed, mirror-like presentation,” it is generally recommended to evaluate an SLA appearance resin or spray-on system.
It is recommended that you refer to the key requirements marked in the 2D drawings/notes. You can also refer to the parameters on this page:
If assembly mating/locating holes are involved, it is recommended to provide STEP + 2D annotations (PDF/DWG) for more accurate evaluation.
We support mainstream 3D/2D project files:
Suggestions for faster and more accurate quotes: Priority provided STEP + 2D annotation(Especially assembly hole locations and critical dimensions).
It is recommended to write clearly in the remarks: Purpose (function/assembly) + quantity + lead time + appearance requirements + critical dimensions, the quote will be closer to your goal.
Commonly used finishing of this material (subject to actual order selection):
If you want something more like the finished product, it's usually recommended to: Sandblasting (unified texture) or Spray painting (greater appearance control), and provide reference pictures is better.
Powder-formed parts usually have a slight granular texture, which is a process characteristic. Common methods for achieving a cleaner appearance:
It can be used for assembly verification and delivery of functional assemblies. It is recommended:
If you have mating surfaces/locating holes/mating structures, it is recommended to provide 2D annotations for a more accurate assessment.
Closed cavities, long and narrow internal channels, and maze-like structures are more prone to powder removal difficulties.
The appearance of the black body is usually more resistant to stains, but when you have higher requirements for "batch consistency/uniform texture", it is recommended:
Delivery time is strongly related to part size, quantity, layout and finishing. Finishing such as sandblasting/painting/threaded inserts will increase labor hours and production scheduling time.
If you need to expedite it, it is recommended to specify in the remarks: Delivery target + acceptable finishing solution + appearance standard, we will give feasible solutions and risk tips.
In order to get a faster and more accurate quote, it is recommended to provide/explain when uploading the file:
You only need three steps: Upload drawings → Confirm project evaluation and quote → Production and delivery after confirmation.