
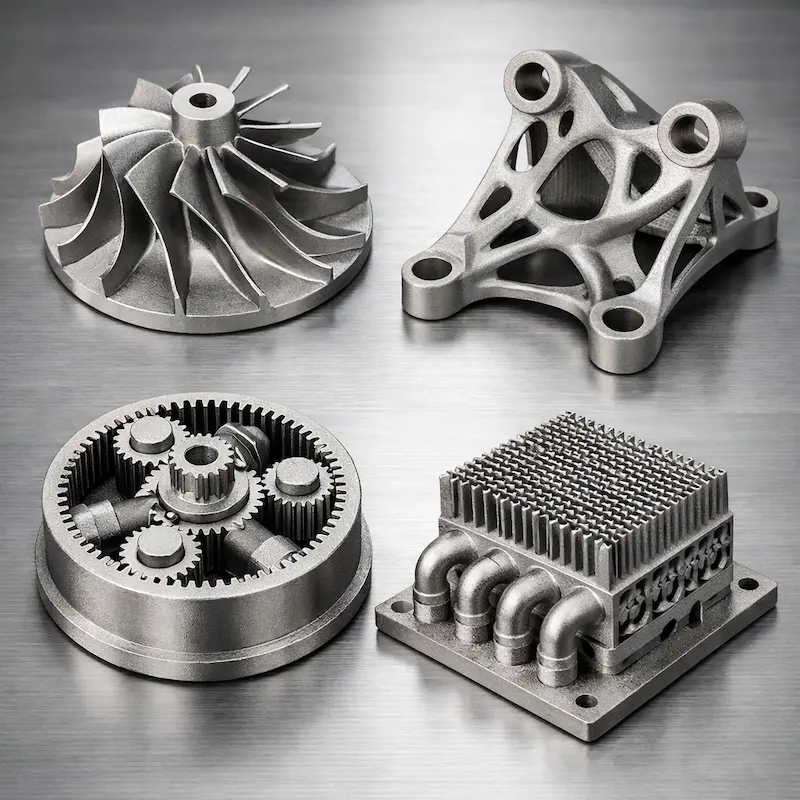
Stainless steel 316L metal 3D printing material (316L stainless steel / SLM 316L / metal additive manufacturing 316L) is suitable for complex structural functional parts, corrosion-resistant environment parts and integrated end-use parts. It supports finishing such as sandblasting and tapping. If necessary, it can cooperate with machining to improve assembly accuracy, and upload files for quick quote and delivery.

316L Stainless Steel

316L Stainless Steel is a very commonly used choice of corrosion-resistant stainless steel in metal 3D printing, suitable for parts you want to have "sufficient strength + corrosion resistance + usable end parts."

Stainless steel (SLM) Corrosion resistant Functional parts/end-use parts Complex structure integrated molding Internal flow channel Can be machined and finished

Quote checklist: Upload your 3D model and, when available, a 2D drawing. Identify the required process, material, quantity, critical dimensions, finish, appearance standard, and target delivery date.

Stainless steel 316L SLM metal 3D printinged sample: corrosion-resistant stainless steel functional parts and end-use parts, supports finishing such as sandblasting and tapping, and can be used with machining to improve assembly accuracy

Key Material and Manufacturing Parameters

Engineering note: Values below are typical reference ranges. Final manufacturability, tolerances, material condition, surface finish, cost, and lead time depend on the drawing, geometry, quantity, and selected process.

Upload CAD files and mark critical features for an engineering review before production.

ProcessSLM metal 3D printing (stainless steel 316L)
Material positioningCorrosion-resistant metal functional parts/end-use parts; suitable for complex structures, integrated designs and internal flow channel parts
Dimensional tolerance (reference)±0.2 mm (common range; it is recommended to process the key hole/datum surface twice or note "precision first")
Minimum wall thickness (reference)≥1.0 mm (Thin-walled/long cantilevers require evaluation of support and deformation control)
Temperature resistance (reference)400℃
Tensile strength (reference)480–650 MPa
Density (reference)7.9 g/cm³
Mounting holes and threads It is recommended to perform secondary processing (enlarging/reaming) on the assembly holes/positioning holes to ensure fit; it is recommended to pass the thread Tapping Obtain more stable assembly quality (please indicate M specification, quantity and location).
Finishing Sand blasting and tapping
Typical lead timeRelated to structural complexity, quantity, support and finishing; clear delivery and expedited options will be given after uploading the file

Finishing

Sandblasting (surface consistency and feel)

Used to improve metal 3D printing surface uniformity, reduce reflection differences, and make the appearance more "industrially consistent". For the exterior surface, please note the sandblasting grade/thickness preference.

Tapping (reliable assembly)

Used to obtain more stable thread assembly quality. Please indicate the thread specification (such as M3/M4/M6), hole position reference and quantity in the remarks.

Why Choose Stainless Steel 316L (Metal 3D Printing)

Corrosion resistant and more stable

It is more stable in humidity, salt spray and some chemical media environments, and is suitable for metal terminals that require long-term reliability.

Solid strength

Suitable for load-bearing structural parts and functional parts; parts sensitive to assembly accuracy can be further improved through secondary processing.

Complex structure integrated molding

It is more suitable for internal structures, special-shaped flow channels and reduced parts assembly design that are difficult to machine with traditional CNC, and improves integration.

Can be combined with finishing and finishing

Supports finishing such as sandblasting and tapping; machining paths for key holes/sealing surfaces can be planned to meet assembly and sealing requirements.

Recommended Applications

  • Resistant to corrosive environments: Humid/salt spray/chemical media, worry about rust or corrosion
  • Complex functional structure: Integrated structure, internal flow channel, reduced parts assembly, lightweight structure optimization
  • End piece delivery: Strength and reliability are given priority, and can be combined with tapping/finishing to complete assembly.
  • Small batch/multi-version iteration: No mold opening required, suitable for rapid iteration verification and small batch delivery

It is not recommended to use it directly (it is recommended to change the plan)

  • Structure is simple and cost sensitive: CNC machining can be evaluated (same appearance/accuracy may be more economical)
  • Ultra high mirror appearance: Requires more complex surface solutions (such as polishing/electrolysis, etc., need to be evaluated separately)
  • Extremely high precision fit: It is recommended to focus on machining, or a combination of printing and finishing.
  • Sealed chambers sensitive to internal powder residues: The design of the powder discharge/cleaning channel needs to be evaluated, otherwise a closed structure is not recommended

Design and DFM Guidelines

  • The inner cavity/runner must be able to discharge powder: Try to provide powder discharge holes and cleaning paths to avoid completely closing the cavity; it is recommended to conduct a DFM review first for complex passages.
  • Recommended secondary processing for key holes/mating surfaces: Printing is more suitable for "forming complex shapes", and key assembly surfaces are more stable through finishing.
  • Thin walls and long cantilevers:≥1.0mm is the reference lower limit; thin-walled/slender structures rely more on support and placement, and it is recommended to reinforce/round corners/shorten the cantilever.
  • Thread priority tapping: It is recommended to tap the threaded holes that require high assembly reliability, and note the thread specifications and quantity.
  • The surface requirements must be stated clearly in advance: Sandblasting can improve the consistency, but roughening of the sealing surface/sliding mating surface needs to be avoided. It is recommended to mark the appearance surface and functional surface.

Comparison with common metal 3D printing materials

Material Key Advantages Mainly applicable Not suitable
Aluminum alloy AlSi10Mg (SLM) Lighter and stronger, suitable for heat dissipation/thermal conduction and complex structure integrated molding Radiator, lightweight bracket, complex flow channel metal parts Strong corrosion resistance is preferred (316L is more stable)
TC4 Titanium (SLM) High strength to weight ratio, corrosion resistance, performance priority High-end structural parts, lightweight end-use parts, and reliability-first parts Budget sensitive, general corrosion resistance needs (316L is more economical)
Die steel 1.2709 (SLM) High strength and good heat treatment performance, suitable for jigs/molds Jigs and fixtures, mold inserts, high-strength structural parts Strong corrosion resistance requirements (316L is more suitable)
Nickel-based superalloy (SLM) Strong high temperature resistance, suitable for high temperature working conditions High temperature functional parts, thermal environment verification parts Only corrosion resistance/general strength needs (316L is more balanced)
White Nylon (SLS) Functional plastic parts, wear-resistant and fatigue-resistant, suitable for batch layout of complex structures Structural validation parts, assembly parts, wear-resistant moving parts Metal Strength/High Temperature Resistance/Metal Corrosion Resistance Terminals

FAQs