
trimming
Trim the edges and outer contour to improve the consistency of feel and appearance; suitable for cosmetic parts and handheld parts.
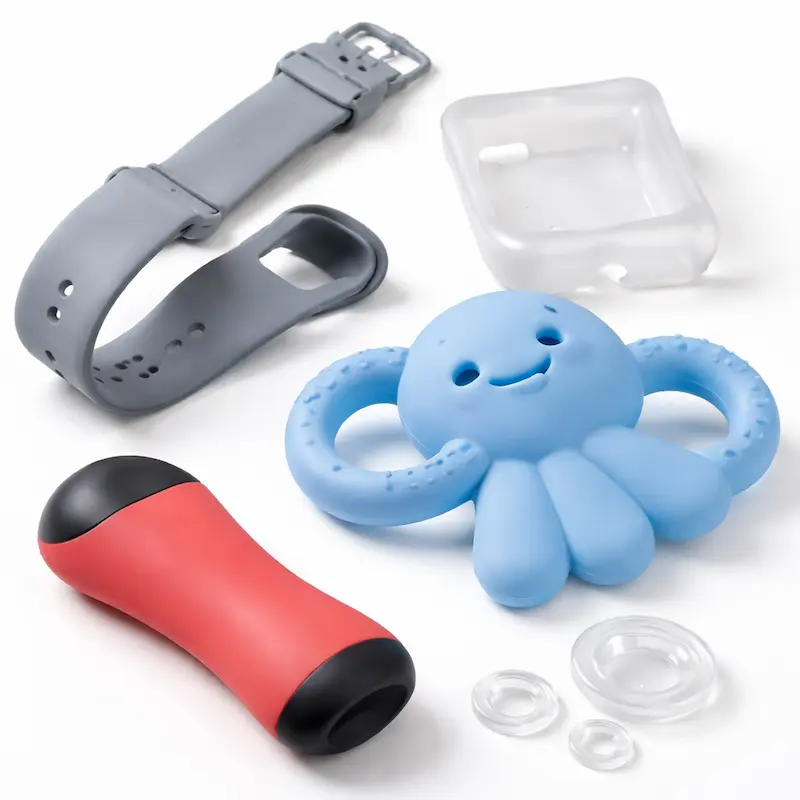
Silicone Rubber series vacuum casting materials are used to create "high elasticity/weather resistance/soft touch" soft prototypes, commonly for seals, waterproofing, shock absorption, and soft-touch components.
Quote checklist: Upload your 3D model and, when available, a 2D drawing. Identify the required process, material, quantity, critical dimensions, finish, appearance standard, and target delivery date.
Engineering note: Values below are typical reference ranges. Final manufacturability, tolerances, material condition, surface finish, cost, and lead time depend on the drawing, geometry, quantity, and selected process.
Upload CAD files and mark critical features for an engineering review before production.
| Process | Vacuum Casting |
|---|---|
| Material type | plastic |
| Material subcategory | soft plastic |
| Accuracy | ±0.2 mm |
| Minimum wall thickness | 1.0mm |
| Service temperature | 300-600℃ |
| Tensile strength | 450-1100MPa |
| Density | 7.7-8.5 g/cm³ |
| Requirements tag | Appearance prototype, flexibility |
| Finishing | Trimming, removing edges, dyeing |
| Typical lead time | Related to structural complexity, quantity, finishing and production scheduling; clear delivery and expedited options will be given after uploading the file |
Trim the edges and outer contour to improve the consistency of feel and appearance; suitable for cosmetic parts and handheld parts.
Clean the parting line and edge to reduce the risk of scratching and improve the assembly experience; it is more important for card slots, sealing edges, etc.
Used to achieve the target color and appearance; it is recommended to provide a color card/reference picture and explain the acceptable range of color difference in the remarks.
Suitable for prototypes and verification parts that require elasticity, cushioning or soft touch; closer to the experience of soft rubber finished products.
Balance between cost, appearance and performance, suitable for staged reviews and small batch verification.
When you need a small number of multiple iterations or a small batch of prototypes, vacuum casting can lower the threshold for trial production and improve response speed.
Supports trimming, stripping and dyeing, making it easier to push the appearance and feel to a more deliverable state.
Silicone (vacuum-cast parts) is more suitable for appearance prototypes and functional validation parts that require flexibility/soft touch, such as hand-feel review samples, soft-touch encapsulation effect verification, buffering/protective structure verification, etc.
It is recommended to describe your target feel and usage conditions in the remarks (whether rebound is required, whether it is under long-term pressure, whether it is in contact with skin/equipment, etc.), and upload reference parts or pictures (if any). The clearer the information, the more accurate the selection and quote will be.
You can refer to the "Accuracy" data (±0.2) on this page. If there are critical assembly dimensions, please provide 2D callouts (PDF/DWG) or mark the critical dimensions in notes, and we will evaluate them individually and confirm accessibility during the DFM stage.
It is recommended to refer to "Minimum wall thickness 1.0mm" on this page. At the same time, try to keep the wall thickness uniform and avoid sudden changes in thickness; if the structure is complex or there are many thin-walled areas, it is recommended to conduct a DFM review first to reduce risks.
The finishing of silicone (vacuum-cast parts) is supported by this material data: Trimming, removing edges, dyeing. If the appearance requirements are high, it is recommended to describe the appearance standards and unacceptable defect types in the remarks.
If dyeing is required, it is recommended to provide a color card/reference picture and explain the acceptable color difference range and usage scenarios (indoor/exhibition lighting/photo studio, etc.). When the consistency requirements are high, it is recommended to produce the products in the same batch and unify the standards.
It is recommended to provide 3D (STEP/STP, IGES/IGS, STL) and critical dimension 2D annotations (PDF/DWG/DXF) first. If there is only STL, please also write down the key dimensions, tolerances and assembly relationships in the remarks.
The main differences usually come from structural complexity, key appearance standards, whether dyeing is required, stripping/edging time, quantity and lead time, etc. It is recommended to upload the file and note the purpose and appearance standards to obtain a quote that is closer to the target.
Common appearance risks include parting lines, edges, edges that are not sharp enough, etc. It is recommended to avoid sharp and thin edges in the design, reserve a reasonable transition for the appearance surface, and clearly indicate the display surface and unacceptable defects in the remarks. We will give optimization suggestions in DFM.
It is recommended to state the following when uploading the file: quantity, purpose (appearance review/functional validation), target feel and working conditions, critical dimensions and tolerances, appearance surface definition, whether trimming/removal/dying is required, lead time and receipt location. The more complete the information, the faster and more accurate the quote and DFM will be.