
polish
Used to remove slight burrs and improve touch; the appearance can be matched with clear acceptance criteria (texture/gloss/feel).
Acetal (POM)(polyoxymethylene, also known as Saigang) is a highly crystalline engineering plastic with excellent rigidity, wear resistance, and dimensional stability.
Quote checklist: Upload your 3D model and, when available, a 2D drawing. Identify the required process, material, quantity, critical dimensions, finish, appearance standard, and target delivery date.
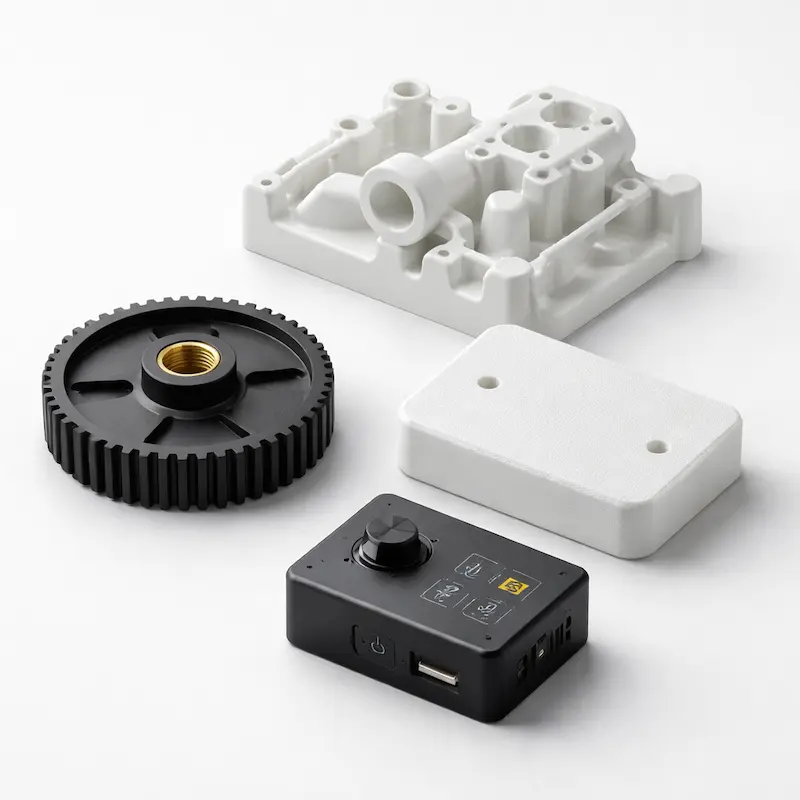
Engineering note: Values below are typical reference ranges. Final manufacturability, tolerances, material condition, surface finish, cost, and lead time depend on the drawing, geometry, quantity, and selected process.
Upload CAD files and mark critical features for an engineering review before production.
| Process | Injection Molding |
|---|---|
| Material | POM (acetal) |
| Accuracy | ±0.2 mm |
| Minimum wall thickness | 1.0mm |
| Service temperature | 300-600℃ |
| Tensile strength | 450-1100MPa |
| Density | 7.7-8.5 g/cm³ |
| Requirements tag | Low-cost universal parts; high surface quality |
| Finishing | Polishing, screen printing, laser engraving, painting |
| Typical lead time | Related to structural complexity, mold plan, quantity and finishing; clear delivery and expedited options will be given after uploading the file |
Used to remove slight burrs and improve touch; the appearance can be matched with clear acceptance criteria (texture/gloss/feel).
Suitable for logos, scales and other graphic information; it is recommended to provide vector files and mark the location and size.
Suitable for serial numbers, QR codes, permanent identification, etc.; please note the engraving content, size and acceptable contrast.
Used to unify color and texture (matte/high-gloss, etc.); it is recommended to provide reference pictures or clarify color numbers and appearance requirements.
It is suitable for scenarios such as prototypes and functional validation, making it easy to make controllable trade-offs between cost and performance.
When you need plastic parts that can be delivered stably and can be produced on a large scale, POM (Sai Gang) is one of the common choices.
The recognition and finished product can be improved through finishing such as polishing, painting, screen printing, and laser engraving.
Upload 3D/2D files to quickly evaluate manufacturability (DFM), quote and lead time.
POM (acetal) injection molding is suitable for scenarios such as prototypes and functional validation. It is also often used for general plastic parts that have a balance between appearance and comprehensive performance.
If you can provide usage conditions, quantity and appearance standards, we can provide material/process suggestions and quotes that are closer to the target.
Key parameters on this page include: accuracy, minimum wall thickness, temperature resistance, tensile strength, density, etc. It is recommended to add the following when placing an order:
The minimum wall thickness given on this page is 1.0mm. Actual manufacturability is also related to part size, flow length, gate location, rib design, etc.
It is recommended to upload the 3D file and note the thin-walled area, and we will give DFM evaluation and optimization suggestions.
It is recommended to provide 3D + 2D combination for faster and more accurate quote:
Cost is usually related to structural complexity, mold solution (with or without slider/inclined roof), appearance grade, quantity and finishing.
The finishing supported by POM (acetal) injection molding is: grinding, screen printing, laser engraving, and painting.
If the goal is a finished product appearance, it is recommended to write clearly in the remarks: paint texture (matte/high-gloss), color requirements (color number/reference picture), position and size of screen printing/laser engraving.
It is recommended that you mark the appearance surface (Side A), prohibited area and acceptance criteria in the drawings or notes. We prioritize optimizing parting line, ejection and gate locations in DFM.
If the appearance requirements are higher, a spray paint scheme can also improve consistency and hide minor marks.
Key practices include: providing 2D tolerances and benchmarks, avoiding sudden changes in thickness, making reasonable round corners on hole edges and strengthening the structure, and reserving secondary processing allowance when necessary.
Once the file is uploaded, we will give you more specific DFM recommendations based on the structure.
Common reasons include: thick meat areas, uneven wall thickness, unreasonable rib design, poor gate location, uneven cooling, etc.
Structural optimization directions usually include: uniform wall thickness, hollowing out thick meat, rationalization of rib locations, rounded corner transitions and appropriate gate/cooling solutions.
It is recommended that you add the following information when uploading the file, which can usually significantly improve the accuracy of the quote: