
Polishing (appearance and feel optimization)
Used to trim parting lines, gate areas and minor surface imperfections; a finer grinding standard can be selected for display surfaces.
ABS effect resin is one of the most commonly used "universal structure + appearance" materials for vacuum casting.
Quote checklist: Upload your 3D model and, when available, a 2D drawing. Identify the required process, material, quantity, critical dimensions, finish, appearance standard, and target delivery date.
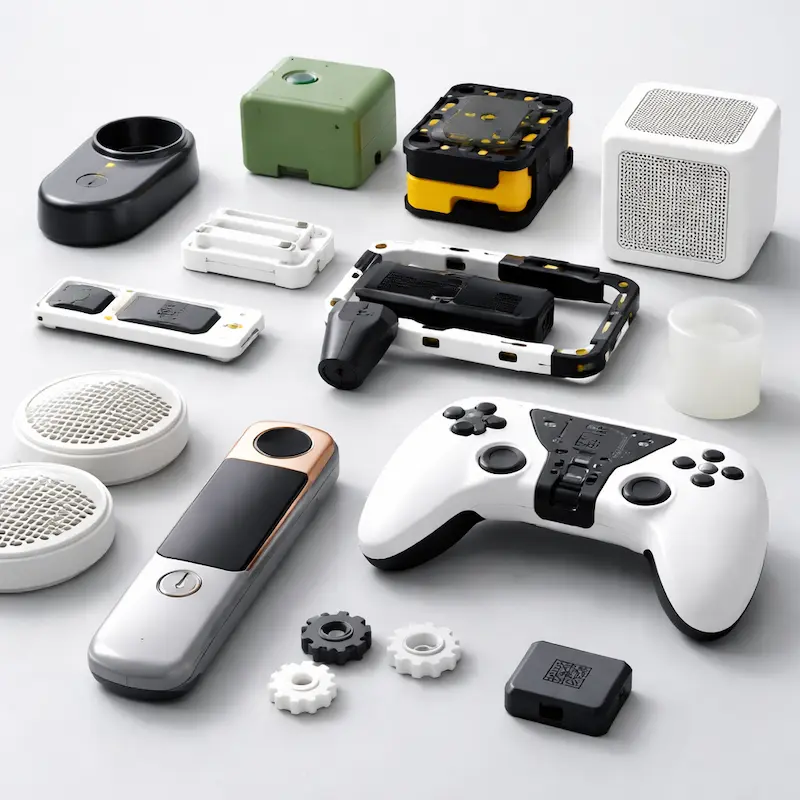
Engineering note: Values below are typical reference ranges. Final manufacturability, tolerances, material condition, surface finish, cost, and lead time depend on the drawing, geometry, quantity, and selected process.
Upload CAD files and mark critical features for an engineering review before production.
| Process | Vacuum casting (silicone mold / small batch replica) |
|---|---|
| Material | ABS |
| Application positioning | Appearance prototype/review sample/small batch reproduction/assembly and functional validation |
| Accuracy | ±0.2 mm (common reference; it is recommended to mark tolerances on key dimensions and confirm with DFM) |
| Minimum wall thickness | 1.0mm (Thinner structures need to assess the risks of pouring and demoulding, and it is recommended to review them first) |
| Service temperature | 300-600℃ (the parameter range is subject to project confirmation and working conditions, it is recommended to indicate the actual operating temperature) |
| Tensile strength | 450-1100MPa (subject to material system/pouring system and project requirements) |
| Density | 7.7-8.5 g/cm³ (subject to material system/project confirmation value) |
| Color | Can be customized (commonly available in similar injection molding colors; for high color consistency requirements, painting is recommended) |
| Surface quality | Achieve better appearance; complex structures/deep cavity areas need to assess the risk of demoulding and surface defects |
| Typical lead time | Relevant to quantity, number of molds, structural complexity and finishing; clear delivery and expedited options will be given after uploading the file |
| Finishing | Polishing, screen printing, laser engraving, painting |
Used to trim parting lines, gate areas and minor surface imperfections; a finer grinding standard can be selected for display surfaces.
It can produce matte/semi-matte/high-gloss effects, etc., which can significantly improve the finished product feeling "like an injection molded part"; it is recommended to provide reference pictures or texture targets.
Suitable for graphic signs on flat or gently curved surfaces; it is recommended to provide vector files and position and size instructions.
Suitable for serial numbers, QR codes, positioning marks, etc.; if the color contrast requirement is high, it can be evaluated together with the spray paint/base color scheme.
Suitable for small batch trial production and multiple rounds of iterations of 5-50 pieces, reducing the threshold and risk of "making a hard mold".
Combined with sanding and painting, a more uniform surface texture can be obtained, which is suitable for review, demonstration and prototype integration.
It can be used for interference inspection, assembly trial assembly and structural first version verification; it is recommended to provide 2D annotations for key hole positions to improve consistency.
Supports screen printing and laser engraving; when a "branded appearance" or stable color difference control is required, priority is given to painting solutions.
Engineering plastics - ABS is often used in appearance prototypes, small batch reproductions, review samples and assembly/function verification, etc. It is especially suitable for the stage where "the appearance of injection molded parts needs to be more similar, but a hard mold is not wanted for the time being".
Vacuum casting is more about "small batch reproduction + appearance closer to injection molding", while 3D printing is more about "rapid prototyping + rapid iteration of structure". If you care more about appearance consistency and batch copying efficiency, engineering plastic-ABS is preferred.
It is recommended to refer to the key requirements marked in the drawings/notes. The dimensional performance of the vacuum casting will be affected by the structure, exhaust, gate and mold life; it is recommended to provide 2D markings for key hole positions/mating surfaces and conduct DFM confirmation first.
Thin-walled structures are more prone to risks such as insufficient pouring, air bubbles and demoulding damage. It is recommended that you indicate the thin-walled area and appearance surface when uploading the file. We will conduct a manufacturability assessment based on the structure and quantity and give optimization suggestions.
Finishing supported by engineering plastics-ABS includes: Polishing, painting, screen printing, laser engraving. Among them, "sanding + painting" is most often used to obtain a more consistent appearance closer to the finished product.
Suggested remarks: Target color (can provide Pantone/reference picture) + gloss (matte/semi-matte/high gloss) + display surface definition. For projects sensitive to color differences, a "spray paint scheme" is recommended first to lock in consistency.
Yes. screen printing More suitable for color-based logos (Logo, scale), Laser engraving More suitable for wear-resistant marking (serial numbers, QR codes). If high contrast and consistency are required, evaluate them together with a spray paint base color.
It is recommended to provide: STEP/STP(preferred) with critical dimensions PDF/DWG/DXF Label the file. Only STL can also be evaluated, but additional 2D annotations are provided for critical hole locations/fitting recommendations to improve quote and manufacturing accuracy.
Vacuum casting quotes are usually related to Structural complexity, molding/mold life, exhaust and demoulding difficulty, finishing requirements, quantity and lead time Related. The higher the appearance standards (painting, fine sanding, marking technology), the higher the labor hours and quality inspection costs.
It is recommended to note the following when uploading files: Quantity, purpose (appearance/assembly/function), appearance standards (whether to spray paint/screen printing/laser engraving), key dimensions/hole position tolerance, display surface definition, lead time and receipt location. The clearer the information, the faster the quote will be confirmed with DFM.